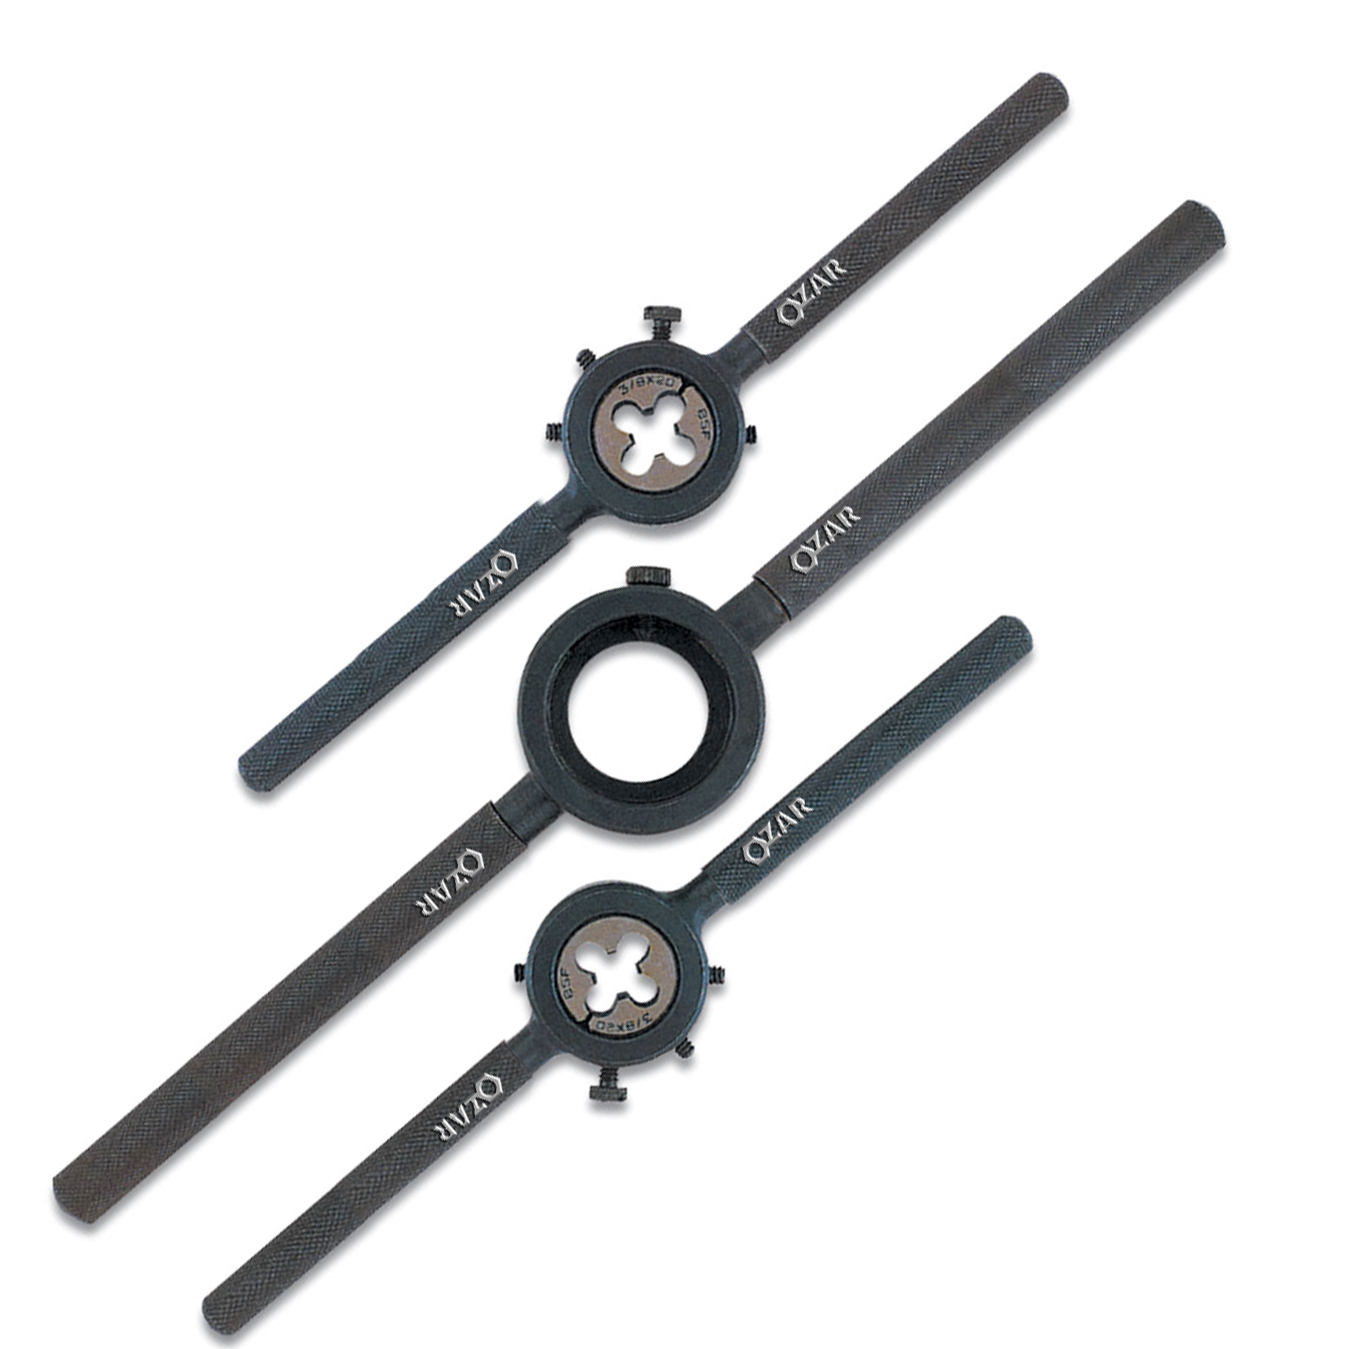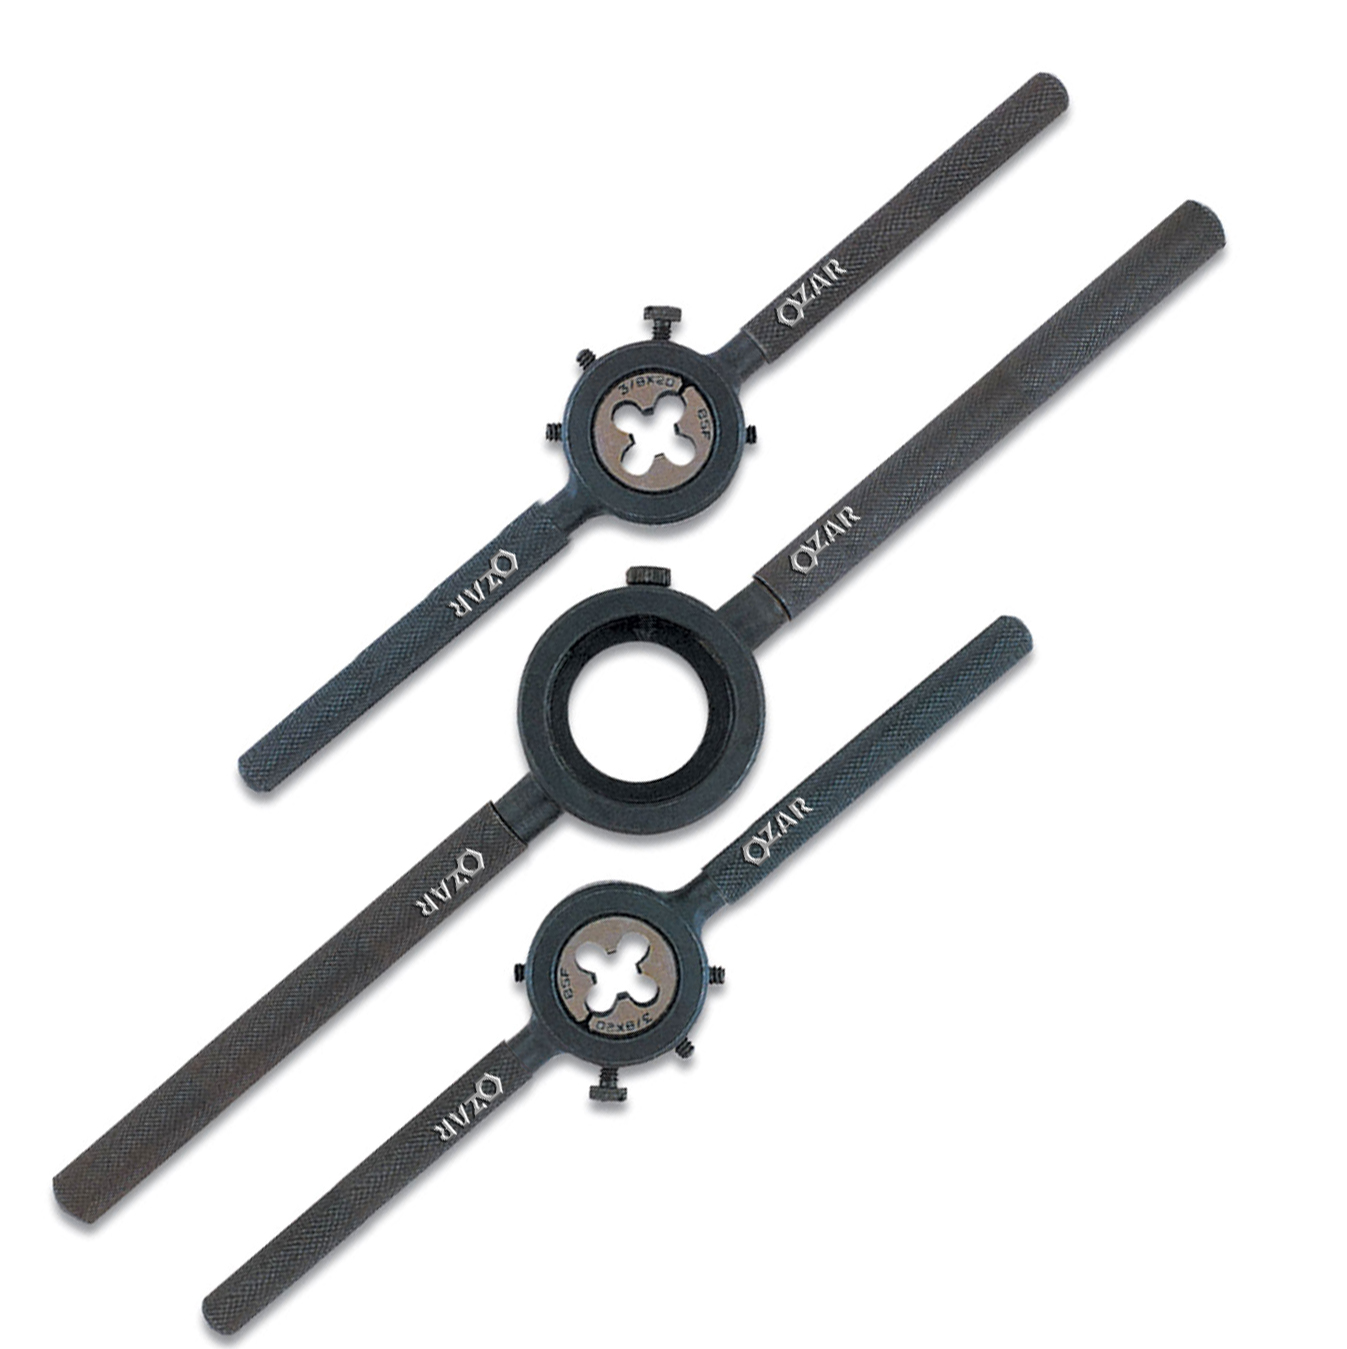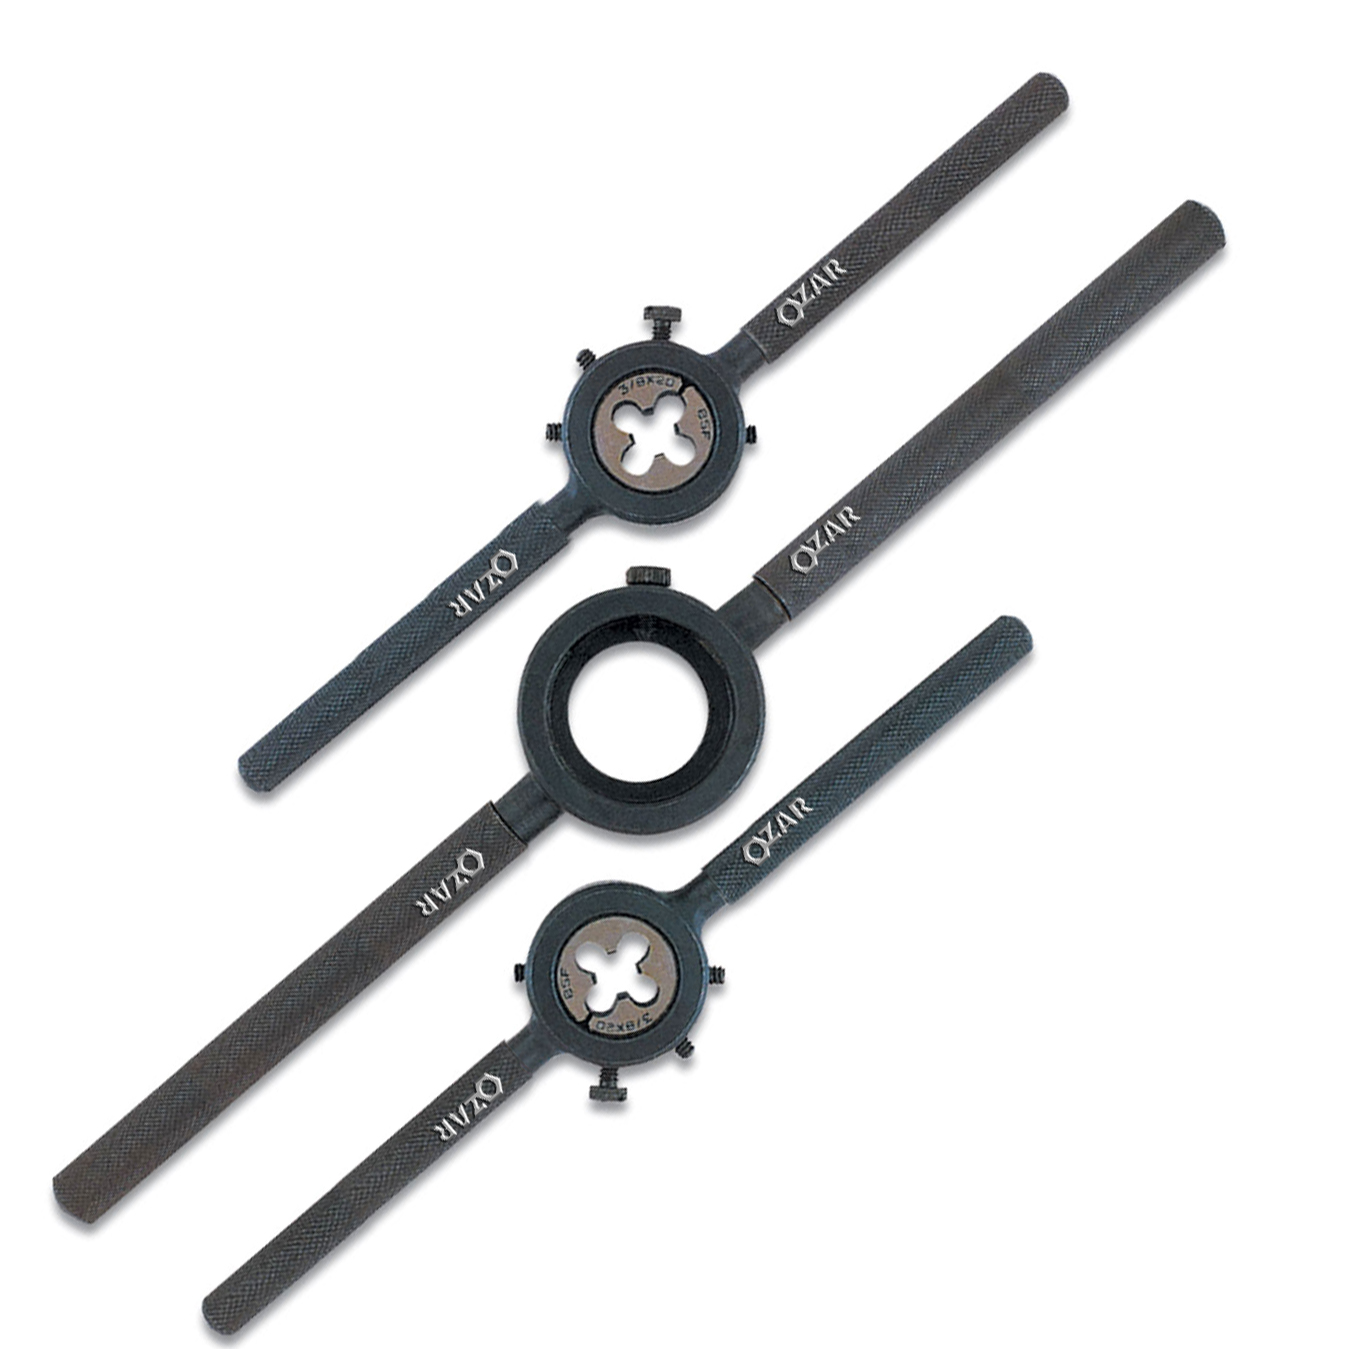
OZAR
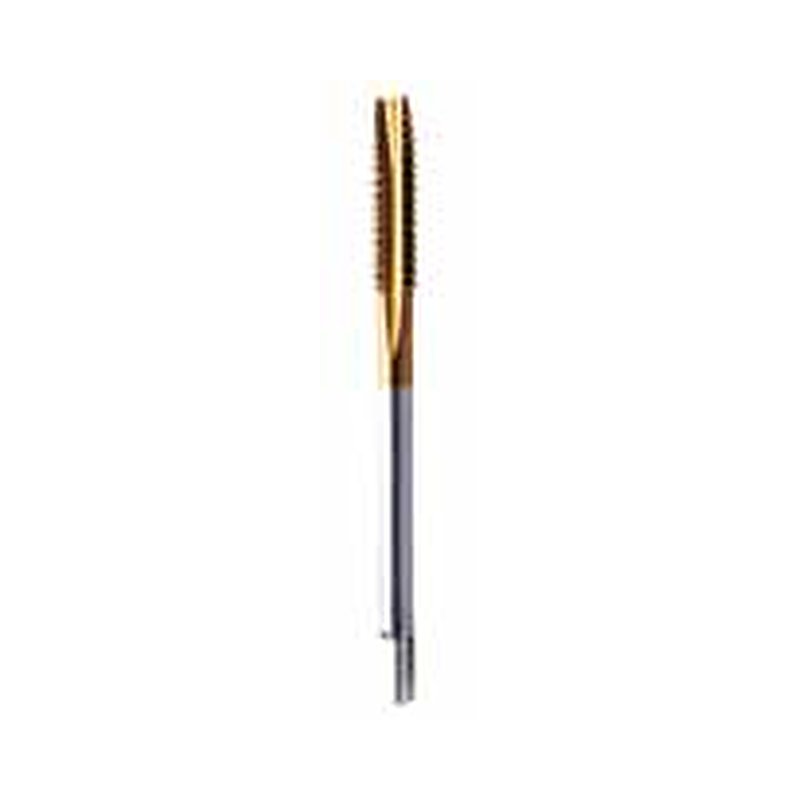
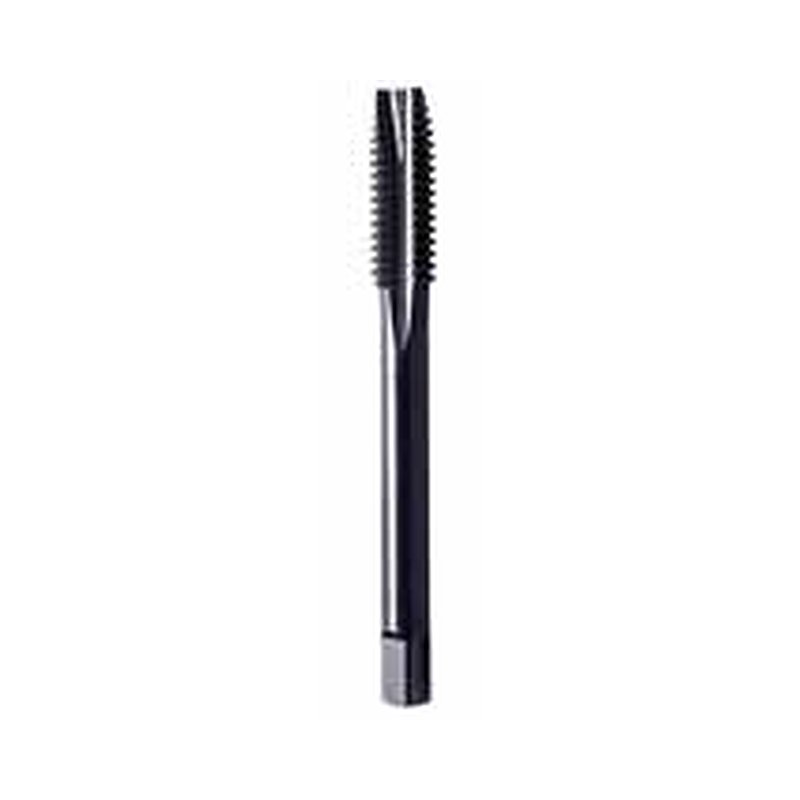
OZAR HSS-E Spiral Point Machine Tap, M3 x 0.5
M3 x 0.548 mm
₹611Was ₹814
Incl. GST
- Ships in 5–7 days
Order online any timeGST invoiceFree delivery above ₹500Talk to us +91 63965 76830 (10 AM–8 PM IST, Mon–Sat)
160 products
₹611Was ₹814
Incl. GST
₹611Was ₹814
Incl. GST
₹624Was ₹832
Incl. GST
₹739Was ₹985
Incl. GST
₹1,128Was ₹1,504
Incl. GST
₹1,708Was ₹2,277
Incl. GST
₹2,058Was ₹2,744
Incl. GST
₹2,279Was ₹3,038
Incl. GST
₹739Was ₹985
Incl. GST
₹739Was ₹985
Incl. GST
₹748Was ₹997
Incl. GST
₹806Was ₹1,074
Incl. GST
₹881Was ₹1,174
Incl. GST
₹5,266Was ₹7,021
Incl. GST
₹819Was ₹1,092
Incl. GST
₹1,836Was ₹2,448
Incl. GST
₹1,976Was ₹2,635
Incl. GST
₹1,859Was ₹2,478
Incl. GST
Showing 121–144 of 160
Taps cut internal threads and dies cut external threads. First identify the thread standard: metric coarse (such as M6 x 1.0 or M12 x 1.75), metric fine, BSW, UNC or UNF. The size and pitch on the tap or die must match the bolt or part you are working with. A hand tap set of 3 pieces (taper, intermediate and plug) is used in sequence for blind and through holes, while spiral point taps push chips forward in through holes and spiral flute taps lift chips out of blind holes.
Choose the material by the job. Carbon steel taps and dies suit occasional hand work in mild steel and soft metals; HSS taps are tougher for regular workshop use, and HSS-E with TiN coating suits machine tapping. Drill the correct tap drill size first, using a thread chart. Use a tap wrench or die stock, keep the tool square, use cutting oil, and turn back often to break chips. Split dies can be adjusted slightly to fine-tune thread fit.
We list OZAR and other brands at prices that include GST, with a GST invoice on every order and delivery across India. Tool rooms, fabricators and maintenance workshops buying several units can ask for a bulk quotation.
Use a plug tap or a spiral flute machine tap, which lifts chips out of the hole. Finish with the plug tap in a 3-piece hand set.
Use a tap drill chart for your thread. For metric coarse threads, the drill size is roughly the thread size minus the pitch, for example 10.2 mm for M12 x 1.75.
Carbon steel taps suit light, occasional hand use. HSS taps last longer and handle harder steel and regular workshop use.
Yes. Prices include GST and every order gets a GST invoice.